Navigation

The C.L. Smith Blog

China Best Graphite Iron Manufacturers and Suppliers

China’s graphite iron industry serves demanding sectors, from pump housings and brake components to agricultural machinery. Graphite Iron combines useful castability with vibration damping and dependable wear performance. However, material selection should never rely on a catalogue photograph alone. Engineers need verified grades, test data, and production evidence.

Experienced Chinese manufacturers typically support gray iron and ductile iron programs with pattern design, molding, melting, machining, and surface treatment. Their capabilities may include spectrometer analysis, tensile testing, hardness checks, and dimensional inspection. Ask for current certificates, not old samples. A reliable supplier can explain its furnace controls, inoculation practice, and defect-prevention methods in practical terms. It should also provide clear tolerances, inspection plans, packing details, and traceability records. Small details matter. A rough casting corner or uneven machined bore can cause costly assembly delays. Site audits, video inspections, and independent testing can strengthen confidence before a large order. Still, no supplier is perfect. Lead times can shift, and advertised capacity may not equal available capacity during peak seasons. This deserves honest discussion.

This guide examines leading China Graphite Iron manufacturers and suppliers through technical capability, quality consistency, communication, and application experience. It considers how each company handles prototypes, repeat production, tooling ownership, and corrective action. Buyers should compare total value rather than the lowest quotation. A cheaper part may require extra machining or fail earlier in service. The right partner listens carefully, documents assumptions, and improves when feedback exposes a weakness. That is where trust becomes measurable.

China Best Graphite Iron Manufacturers and Suppliers

Graphite Iron: Definition, Properties, and Industrial Applications

China Best Graphite Iron Manufacturers and Suppliers

Graphite iron is cast iron containing carbon in graphite form. Its structure controls strength, vibration damping, machinability, and wear resistance. Flake graphite creates gray iron, while spherical graphite produces ductile iron. These forms behave differently under load.

In practical foundry work, graphite shape matters as much as chemical composition. Gray iron absorbs vibration well, making it useful for machine bases, brake components, and engine housings. Ductile iron offers higher toughness for pipes, gears, suspension parts, and agricultural machinery. Its performance depends on cooling rate, heat treatment, section thickness, and casting quality. A part can meet a strength target yet fail from porosity or poor graphite distribution. No grade is perfect.

Tips: Ask manufacturers and suppliers for chemical analysis, tensile results, hardness data, and metallographic images. Confirm dimensional tolerances, surface finish, and inspection methods before placing an order. Sample testing is wise, although it adds time and cost. Check whether production controls remain stable across repeated batches. A reliable supplier should explain defects openly and provide traceable inspection records. This is often more valuable than a low quotation. Supplier claims still need independent verification.

Types of Graphite Iron Products and Their Manufacturing Processes

Graphite iron products vary by graphite shape, matrix structure, and service demand. Gray iron contains flake graphite, offering good vibration damping and machinability. Ductile iron uses spherical graphite, which improves strength and impact resistance. Compacted graphite iron sits between both types. It provides useful thermal conductivity and moderate mechanical performance. These materials serve in pump housings, brake components, engine blocks, pipes, and industrial frames.

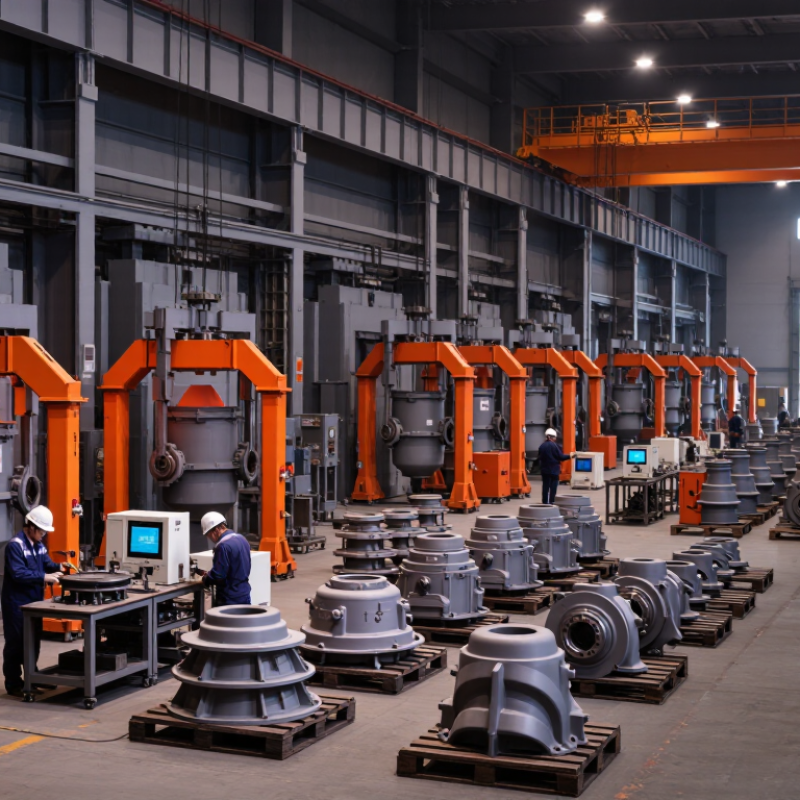
Manufacturing begins with melting selected iron, steel scrap, carbon, and alloy additions in an electric or cupola furnace. Technicians control temperature and chemical composition before pouring. Inoculation encourages the desired graphite structure. Ductile iron also requires magnesium treatment, followed by careful slag removal. Molten metal enters sand, shell, or permanent molds. After solidification, workers remove runners, clean surfaces, and heat-treat selected parts. Machining then creates accurate holes, faces, and mounting points. Quality checks may include hardness testing, tensile testing, dimensional inspection, and metallographic analysis. A minor chemistry error can change graphite shape. That risk deserves attention.

Tips: Match the iron type to the load, temperature, and vibration level. Check graphite morphology, not only surface appearance. Ask suppliers for melt records, test results, and traceable inspection data. Test sample castings before approving large production runs. This step may feel slow, but it often prevents expensive failures. Also review wall thickness carefully. Thin sections can cool too quickly and produce inconsistent properties. No process is flawless. Experienced manufacturers still investigate defects, adjust parameters, and document every corrective action.

How to Evaluate Graphite Iron Manufacturers and Suppliers in China

Evaluating graphite iron manufacturers in China requires more than comparing quotations. In practical sourcing, inspect the melting process, inoculation method, and nodularizing treatment. Ask for recent chemical-analysis records, not only polished samples. Carbon equivalent, sulfur, magnesium, and silicon levels strongly affect graphite shape and casting performance.

The USGS Mineral Commodity Summaries 2024 reported about 1.6 million metric tons of natural graphite production worldwide in 2023. China remained the leading producer, but scale does not prove foundry quality. Use ISO 1083 or EN 1563 requirements when reviewing ductile iron grades. Request tensile strength, elongation, hardness, and metallographic results from the same production batch. Check whether independent laboratories performed these tests. Small details matter.

Audit the factory floor. Look for calibrated spectrometers, controlled furnace temperatures, sand-testing equipment, and traceable heat numbers. Review defect rates, corrective-action reports, and dimensional inspection records. A supplier should explain how it handles shrinkage, porosity, and graphite degeneration. Vague answers deserve caution. Very low prices often exclude testing or tooling maintenance.

An on-site audit helps.

Still, no audit is perfect. Confirm capacity with a pilot order, then compare results against approved drawings and acceptance criteria. The IEA’s Global Critical Minerals Outlook 2024 notes China’s dominant role in graphite processing, yet processing strength should not replace supplier verification. Supplier resilience also requires backup raw-material channels, realistic lead times, and clear packaging controls. The best evaluation remains evidence-based, repeatable, and willing to question attractive assumptions.

Quality Standards, Testing Methods, and Certification Requirements

China Best Graphite Iron Manufacturers and Suppliers

Quality in graphite iron starts with a controlled melt, not a polished certificate. Experienced suppliers should record furnace temperature, inoculant additions, chemical composition, and pouring time for every lot. ASTM A48 and ISO 185 commonly guide gray iron grades, while ASTM A536 and ISO 1083 cover spheroidal graphite iron. Chemistry alone is not enough. Graphite shape matters.

A reliable testing plan combines spectrometer analysis, tensile testing, hardness checks, and metallographic inspection. Inspectors should examine graphite flakes or nodules under a microscope, checking size, distribution, and matrix structure. Dimensional inspection and pressure testing may also be necessary for pump bodies and hydraulic parts. EN 10204 3.1 documentation can link results to a specific heat number. The ISO Survey 2023 reported more than 1.2 million ISO 9001 certificates worldwide, showing how widely process certification is used. Yet certification does not replace physical evidence.

Tips: Request a sample inspection report before ordering. Ask for heat numbers, test dates, equipment calibration records, and acceptance limits. Compare the report with ASTM, ISO, or customer drawings. A weakness often appears here: some documents list “passed” without measured values. Require the numbers. Suppliers should also explain rejected castings, corrective actions, and retest rules. This small detail reveals whether quality control is practiced or merely documented.

China Best Graphite Iron Manufacturers and Suppliers - Quality Standards, Testing Methods, and Certification Requirements
Quality Dimension Applicable Standard or Grade Typical Requirement or Reference Value Testing Method Recommended Supplier Evidence
Material Classification ISO 1083 / EN 1563 Graphite iron with spheroidal graphite is commonly specified as ductile cast iron. The material designation should identify the required mechanical property class and, where applicable, the impact or matrix requirement. Metallographic examination combined with mechanical testing and chemical analysis. Material specification, heat number, charge records, and traceable inspection report.
ASTM Mechanical Grade ASTM A536 Common reference grades include 60-40-18: minimum tensile strength 60 ksi (approximately 414 MPa), yield strength 40 ksi (approximately 276 MPa), and elongation 18%. Tensile test using a calibrated universal testing machine. Heat-specific tensile test report stating specimen location, dimensions, test temperature, and results.
Higher-Strength ASTM Grade ASTM A536 Common reference grades include 65-45-12: minimum tensile strength 65 ksi (approximately 448 MPa), yield strength 45 ksi (approximately 310 MPa), and elongation 12%. Tensile testing in accordance with the applicable ASTM requirements. Test certificate linked to the casting heat and the production lot.
Strength and Ductility EN 1563 / ISO 1083 Typical EN-GJS grades include EN-GJS-400-15 and EN-GJS-500-7. The first number represents the nominal minimum tensile strength in MPa, while the second represents the nominal minimum elongation percentage. Actual requirements depend on grade and section thickness. Room-temperature tensile test on separately cast or cast-on specimens, as specified by the order and standard. Mechanical property report showing grade, section category, specimen type, and acceptance criteria.
Yield Strength ISO 6892-1 / ASTM E8/E8M Yield strength or proof strength must meet the value specified for the selected material grade. The applicable definition should be stated, such as yield point or 0.2% proof strength. Extensometer-based tensile testing with controlled loading rate. Machine calibration certificate, stress-strain data, and test result summary.
Hardness ISO 6506-1 / ASTM E10 Hardness limits are normally agreed according to the grade, matrix structure, and application. Brinell hardness is widely used for ductile iron castings. Brinell hardness testing, normally using a carbide ball and specified test force. Hardness map showing measurement locations, values, surface preparation, and equipment identification.
Impact Toughness ISO 148-1 / EN 1563 Impact energy requirements apply when a grade or purchase specification includes impact toughness. The test temperature and minimum absorbed energy must be defined in advance. Charpy V-notch impact test at the specified temperature. Impact test report including notch orientation, test temperature, individual values, and average value.
Graphite Shape and Distribution ISO 945-1 For spheroidal graphite iron, graphite should predominantly appear as compact or nodular particles. Nodularity, particle count, size distribution, and graphite degeneration should be controlled according to the agreed specification. Metallographic preparation, optical microscopy, image analysis, and comparison with reference classifications. Microstructure photographs, nodularity percentage, particle count, and evaluation magnification.
Matrix Structure ISO 1083 / EN 1563 The ferrite-pearlite balance, carbide content, and other matrix features should be compatible with the required strength, ductility, wear resistance, and machinability. Etched and unetched metallographic examination, usually with optical microscopy. Metallographic report identifying matrix constituents and any carbides, inclusions, or abnormal structures.
Chemical Composition Purchasing Specification / Grade Standard Carbon, silicon, manganese, sulfur, phosphorus, magnesium, and alloying elements should remain within the approved range for the selected grade and casting process. Limits are grade- and application-dependent rather than universal. Optical emission spectroscopy or X-ray fluorescence, with thermal analysis where process control requires it. Heat chemistry certificate, spectrometer calibration status, and furnace charge traceability.
Dimensional Accuracy ISO 8062-3 Dimensional tolerances should be agreed by the required casting tolerance grade, drawing requirements, machining allowance, datum structure, and inspection method. Coordinate measuring machine, calibrated gauges, vernier instruments, or dedicated fixtures. Dimensional inspection report with drawing revision, measured dimensions, tolerances, and equipment details.
Surface Quality Drawing and Purchase Specification Castings should be free from unacceptable cracks, cold shuts, misruns, harmful shrinkage, excessive sand adherence, and other discontinuities defined as rejectable by the drawing or quality plan. Visual inspection, surface profile checks, and dimensional verification after cleaning or shot blasting. Visual acceptance criteria, inspection checklist, photographs where required, and nonconformance records.
Internal Soundness ASTM E446 / ASTM E280 or Customer Specification Internal shrinkage, porosity, inclusions, and other discontinuities must remain within the acceptance level specified for the component's function and critical areas. Radiographic testing, ultrasonic testing, or other approved volumetric examination. NDT procedure, operator qualification, inspection coverage, image or scan records, and acceptance evaluation.
Surface Crack Detection ASTM E1417/E1417M / ISO 3452-1 Liquid penetrant testing is suitable for detecting open-to-surface discontinuities on appropriately prepared, non-porous surfaces. Visible or fluorescent penetrant inspection after cleaning, dwell, removal, and developer application. NDT report identifying inspected areas, penetrant system, acceptance criteria, and qualified personnel.
Magnetic Particle Inspection ASTM E1444/E1444M / ISO 9934-1 Magnetic particle testing can detect surface and near-surface discontinuities in ferromagnetic ductile iron castings. Dry or wet magnetic particle examination using a calibrated yoke or suitable magnetizing equipment. Procedure qualification, equipment verification, inspection map, indications record, and acceptance decision.
Pressure or Leak Integrity Customer Drawing / Application Standard Pressure-retaining castings should meet the specified hydrostatic, pneumatic, or functional leak-tightness requirement. Pressure, holding time, medium, and allowable leakage must be documented. Hydrostatic pressure test, air-under-water test, pressure-decay test, or helium leak test where specified. Pressure-test record showing test pressure, duration, equipment identification, and result.
Heat Treatment Approved Process Specification Heat treatment may be required to obtain a specified ferritic, pearlitic, austempered, or stress-relieved structure. The cycle must be validated for the casting geometry. Recorded furnace temperature, time-at-temperature, cooling rate, and post-treatment mechanical or microstructural verification. Furnace chart, batch identification, thermocouple calibration, and heat-treatment certificate.
Quality Management Certification ISO 9001 ISO 9001 certification demonstrates that the organization operates a documented quality management system. It does not by itself certify a particular casting grade or guarantee product conformity. Assessment and surveillance audit by an accredited certification body. Valid certificate, scope of certification, issuing body, certificate number, and expiry date.
Environmental Management ISO 14001 ISO 14001 addresses environmental management processes, legal compliance controls, and continual improvement. It is generally a supplier-management qualification rather than a material-performance certificate. Certification audit and periodic surveillance audit. Valid certificate and clearly stated site and activity scope.
Occupational Health and Safety ISO 45001 ISO 45001 covers occupational health and safety management systems, including hazard identification and operational controls. Third-party management-system audit. Valid certificate showing the certified manufacturing location and scope.
Material Traceability EN 10204 Inspection documents may be supplied as an inspection certificate or inspection report. A 3.1 certificate generally provides manufacturer-declared, batch-specific results; a 3.2 certificate involves additional validation by an authorized representative or purchaser's representative. Review of heat numbers, production records, test results, and document signatures. Traceable EN 10204 inspection document linked to the casting lot and purchase order.
Regulatory Compliance Application-Dependent Requirements Pressure equipment, machinery, automotive, rail, food-contact, drinking-water, and construction applications can impose different regulatory or customer requirements. Certification should be selected according to the final use and destination market. Conformity assessment, product testing, technical-file review, or third-party approval as required by the applicable regulation. Declaration of conformity, applicable approvals, test reports, risk assessment, and technical documentation where required.
Supplier Prequalification Customer Quality Agreement A qualified supplier should demonstrate stable melting, inoculation, spheroidization, molding, heat-treatment, machining, inspection, and corrective-action processes. Process audit, sample approval, capability review, first-article inspection, and periodic performance monitoring. Process flow chart, control plan, PFMEA, inspection plan, capability data, corrective-action procedure, and audit records.
Note: Mechanical values, dimensional tolerances, NDT acceptance levels, chemical limits, and certification requirements must be confirmed against the selected grade, casting section thickness, drawing, application, destination market, and purchase specification.

China’s Graphite Iron Supply Chain, Customization, and Export Services

China’s graphite iron supply chain combines foundries, pattern makers, machining workshops, and export agents. Experienced suppliers usually confirm grade, hardness, tensile strength, and application before quoting. They review drawings, 3D files, tolerances, and production volumes. This reduces costly changes after tooling begins.

Customization may include casting geometry, wall thickness, machining allowances, surface treatment, and packaging. A reliable supplier should provide sample approval, material reports, dimensional inspection, and batch traceability. Independent testing can support quality decisions for critical components. Still, the process is not always smooth. A small detail in a drawing can affect casting stability, delivery time, or final cost.

Tips: Request a complete technical quotation. Ask about tooling ownership, inspection equipment, lead times, and replacement policies. Confirm whether prices include machining, export packing, and inland transport. Check how defects are recorded and corrected. Keep communication in writing.

For export orders, suppliers commonly prepare commercial invoices, packing lists, certificates of origin, and shipping documents. They should also explain loading methods, moisture protection, pallet limits, and port schedules. Heavy graphite iron parts need secure packing to prevent impact damage and rust during transit. Delivery planning should include production buffers, especially during busy seasons. Some buyers focus only on unit price, which can be a mistake. Total landed cost matters more.

Back to top