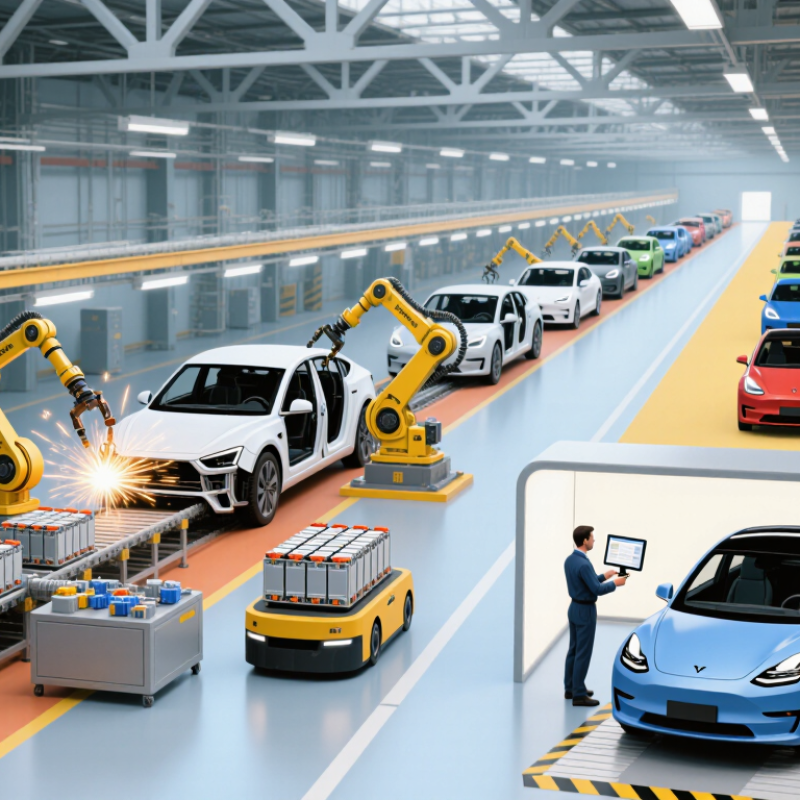
| 1. Map the complete cell-to-pack flow | Show the route from incoming cell inspection through cell grouping, electrical connection, module or cell-stack assembly, pack enclosure, electrical testing, and end-of-line release. Include rework loops and material handoffs. | For each station, record process time, buffer capacity, operator tasks, equipment interface, and quality check. Identify where the design uses a module-based route or a cell-to-pack route. | Request a station-by-station flow diagram and a layout showing people, product, and material movement before approving the line concept. |
| 2. Define the dry-room boundary and dew-point requirement | Identify every operation where moisture-sensitive battery materials or exposed cells require controlled humidity. Specify a battery dry-room dew point of ≤−40°C for the applicable production zones. | State the measurement locations, operating condition, alarm limits, monitoring frequency, recovery procedure, and records. Verify conditions at the product or process area, not only at the air-handling unit. | Define the required dew point at the point of use and during normal production. Confirm that doors, pass-throughs, personnel entry, and material transfers are included in the moisture-load assessment. |
| 3. Size capacity from demand and available production time | Translate the required annual good-pack volume into a required line rate using the planned shifts, operating days, scheduled hours, and expected yield. | A basic planning relationship is: required gross output rate = required good output ÷ planned production time ÷ expected yield. Validate cycle time at the constraint station and account for changeovers and planned downtime. | Ask suppliers to show the assumptions behind their capacity figures and to identify the bottleneck, parallel equipment, and buffer strategy. |
| 4. Specify cell handling and joining processes | Describe cell identification, orientation, positioning, clamping, busbar or connector joining, insulation placement, and inspection. Match the process to the selected cell format and pack architecture. | Specify process windows and verification methods for critical operations, such as weld monitoring, dimensional checks, electrical continuity, and insulation checks where applicable. | Require trials with representative cells and components. Confirm that tooling accommodates approved tolerances and that failed or suspect cells can be safely segregated. |
| 5. Build quality checks and traceability into the route | Link cell, component, process, and pack records through a unique identifier. Define inspection gates, nonconformance handling, rework authorization, and final release criteria. | List the data to capture at each operation, such as cell IDs, equipment and recipe IDs, timestamps, process results, operator or system status, and test outcomes. | Demonstrate a complete genealogy record for a sample pack, including how the system prevents unapproved parts or failed process steps from advancing. |
| 6. Plan battery safety and abnormal-event controls | Review hazards and controls for cell storage, handling, electrical testing, charging or discharging steps, thermal events, and damaged-cell isolation. Coordinate design with site safety and applicable regulations. | Document risk assessments, emergency stops, guarded equipment, electrical isolation, detection and alarm interfaces, safe storage arrangements, and response procedures as applicable to the process. | Require a process-specific safety review and clear ownership for integrating equipment safeguards with facility alarms and emergency response plans. |
| 7. Check utilities, maintainability, and acceptance criteria | List electrical power, compressed air, cooling, exhaust, network, floor space, access, and dry-room interfaces. Define routine maintenance and calibration needs for production and measurement equipment. | Agree on commissioning and acceptance tests for safety, cycle time, quality checks, traceability, uptime measurement, and the specified dry-room dew point under stated operating conditions. | Use measurable, documented acceptance criteria and require training, spare-parts information, maintenance instructions, and handover of equipment and process records. |