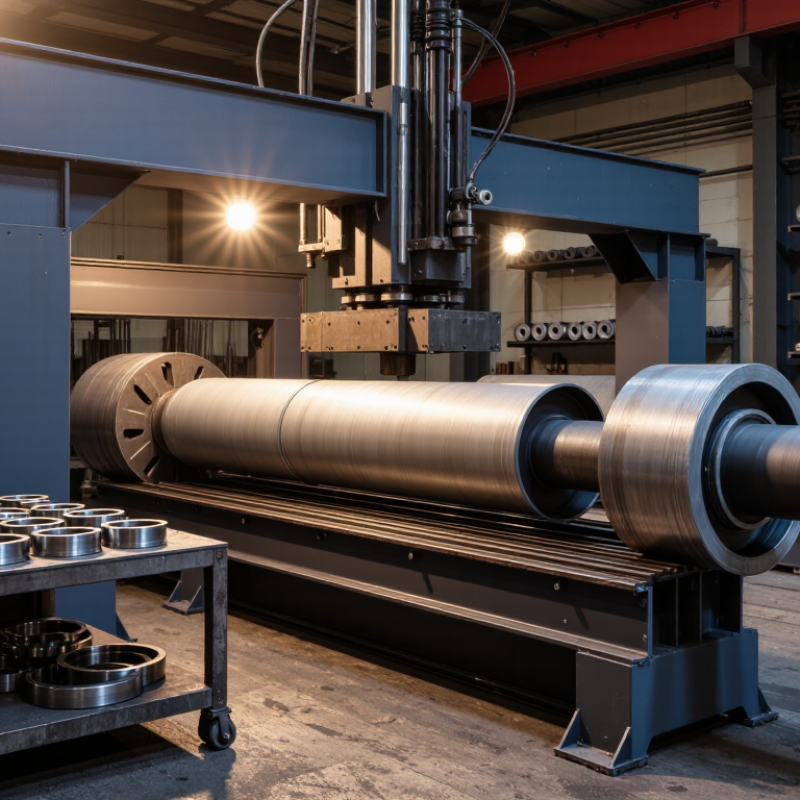
| Definition | Pipe ring bending machine | A machine that forms straight pipes or tubes into circular rings, arcs, coils, or other curved profiles by applying controlled bending force through rolls, dies, or hydraulic tooling. | It produces repeatable curved components while reducing deformation, wrinkling, and dimensional variation compared with manual bending. |
| Primary forming method | Roll bending | Uses three or more rolls to progressively curve the pipe. Suitable for large-radius rings, arcs, and continuous production. | Provides gradual forming and is generally suitable when a smooth radius and low surface damage are required. |
| Primary forming method | Rotary-draw bending | Uses a bend die, clamp die, pressure die, and mandrel when necessary to form a fixed-radius bend. | Offers accurate radius control and is effective for smaller radii, tight bends, and applications requiring consistent geometry. |
| Machine type | Manual or hand-operated | Best for light-duty work, prototypes, repairs, and occasional production. Capacity depends strongly on pipe material, wall thickness, and tooling. | Lower purchase and maintenance cost, but higher operator effort and lower repeatability than powered systems. |
| Machine type | Hydraulic | Uses hydraulic cylinders to generate high forming force. Commonly selected for medium- to heavy-wall steel or stainless-steel pipe. | Provides high force and stable forming performance for larger diameters and thicker walls. |
| Machine type | CNC or programmable | Uses programmed bending angles, feed lengths, rotation, and repeat cycles. Often includes automatic positioning and recipe storage. | Best for repeated production, complex shapes, reduced setup variation, and improved dimensional consistency. |
| Pipe diameter | Required working range | Specify the minimum and maximum outside diameter that the machine and tooling must support. Common machine ranges extend from small tubing to large structural pipe. | A machine rated only for a narrow diameter range may require additional tooling or may not be suitable for future projects. |
| Wall thickness | Required material range | Confirm the minimum and maximum wall thickness for carbon steel, stainless steel, aluminum, copper, or other specified materials. | Thin-wall pipe is more vulnerable to flattening and wrinkling, while thick-wall pipe requires greater forming force. |
| Minimum bending radius | Centerline-radius capability | Choose tooling based on the required centerline radius. The practical minimum radius depends on outside diameter, wall thickness, material strength, tooling, and whether a mandrel is used. | A smaller radius generally increases the risk of ovalization, wall thinning, wrinkling, or cracking. |
| Dimensional quality | Roundness and springback control | Look for adjustable roll pressure, calibrated tooling, controlled over-bending, and programmable compensation where precise ring dimensions are required. | Elastic springback causes the pipe to open slightly after forming; compensation improves final accuracy. |
| Tooling requirement | Dies, rolls, guides, and mandrels | Tooling should match the pipe outside diameter, profile, material, wall thickness, and target radius. Dedicated tooling is often used for repeated sizes. | Correct tooling supports the pipe, limits surface marking, and helps maintain the intended cross-section. |
| Production volume | Low-volume or prototype work | Manual or basic hydraulic equipment may be sufficient when changeovers are frequent and output requirements are limited. | Simple equipment can reduce initial cost when automation and high cycle rates are unnecessary. |
| Production volume | Medium- and high-volume work | Hydraulic, servo-assisted, or CNC equipment is generally more suitable for repeat orders and multiple identical rings. | Powered automation reduces cycle time, operator fatigue, and variation between parts. |
| Main application | Handrails, guardrails, and architectural structures | Used for curved railings, ramps, entrance features, canopy frames, and decorative metalwork. | These applications often require smooth appearance, consistent curvature, and minimal surface marking. |
| Main application | Automotive and transport components | Used for exhaust sections, chassis members, protective bars, vehicle frames, and other tubular components. | Accurate geometry helps ensure proper fit, clearance, weld alignment, and repeatable assembly. |
| Main application | Industrial piping and process equipment | Used for pipe loops, supports, manifolds, heat-transfer layouts, and fabricated piping sections. | Controlled bending can reduce the number of joints and fittings, but the final design must still satisfy applicable piping requirements. |
| Main application | Boilers, heat exchangers, and energy equipment | Used for tube coils, heating circuits, cooling circuits, and curved connections made from suitable metals. | Accurate spacing and bend geometry support efficient installation and reliable fluid flow. |
| Main application | Furniture, lighting, and fitness equipment | Used for chair frames, table bases, lamp structures, exercise equipment frames, and tubular consumer products. | These products typically require repeatable shapes, clean surfaces, and attractive finished appearance. |
| Safety and maintenance | Operational requirements | Prioritize guarding, emergency stops, overload protection, clear tooling access, lubrication points, and operator training. | Safe machine design and regular maintenance reduce injury risk, unplanned downtime, and tooling damage. |
| Best selection rule | Match the machine to the complete job specification | Evaluate pipe material, outside diameter, wall thickness, target radius, ring diameter, production volume, tolerance, surface requirements, available tooling, and floor space. | The best machine is not necessarily the largest one; it is the model that covers the required range with adequate force, accuracy, safety, and operating efficiency. |