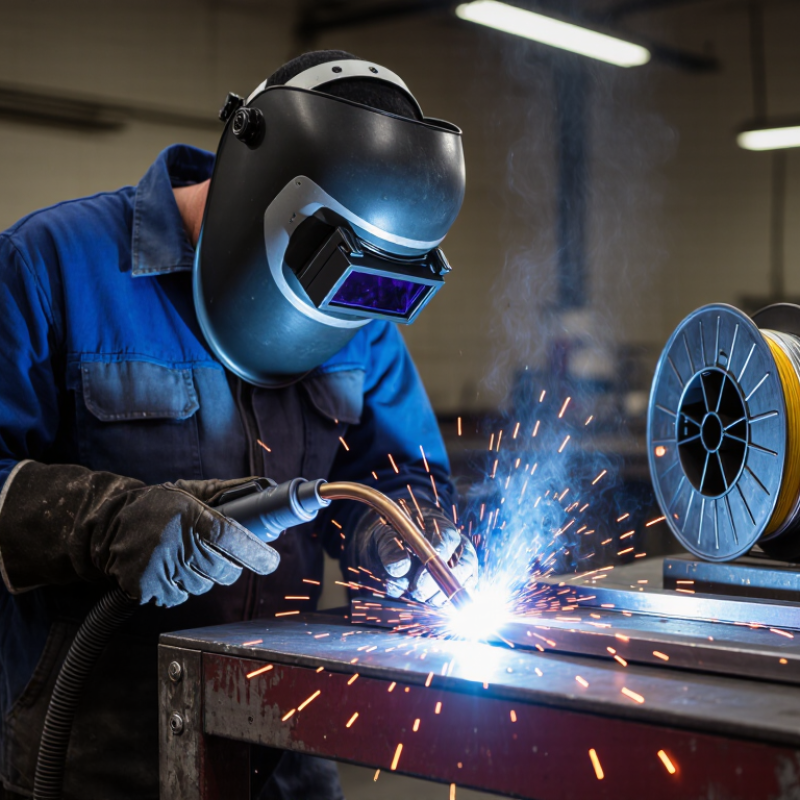
| Voltage | About 17–20 V for short-circuit welding of 1/8 in (3 mm) mild steel. | Voltage primarily affects arc length and bead profile. Too little can cause a short, erratic arc; too much can make the arc harsh and increase spatter or undercut. | Adjust in small increments while maintaining a steady arc. Recheck the wire-feed setting because the two settings work together. |
| Wire-feed speed | Common starting range: 180–260 in/min with 0.030 in wire, or 150–230 in/min with 0.035 in wire. | Wire-feed speed largely controls welding current and deposition rate. Too slow can cause a weak, unstable arc; too fast can produce excessive stubbing, spatter, or an overly large bead. | Use the machine chart or qualified welding procedure as the primary reference. Tune wire feed and voltage together for a smooth, consistent arc. |
| Shielding gas and flow | A common mild-steel short-circuit mixture is 75% argon / 25% carbon dioxide, at approximately 20–30 CFH (9–14 L/min) indoors. | Insufficient shielding or drafts can cause porosity. Excessive flow can create turbulence that draws air into the shielding envelope. | Check for leaks, keep the nozzle clear, and protect the weld area from drafts. Follow the gas and procedure requirements for the material and transfer mode. |
| Polarity | DCEP (direct current electrode positive) is commonly used for solid-wire MIG welding. | Incorrect polarity can result in an unstable arc, excessive spatter, and poor fusion. | Confirm the power-source polarity matches the wire and welding procedure before striking an arc. |
| Contact-tip-to-work distance (CTWD) | Approximately 3/8–1/2 in (10–13 mm) is a common short-circuit starting range. | A longer distance can reduce current and make arc control less consistent; a shorter distance can increase current and risk contact-tip damage or wire burnback. | Keep the distance steady and use the procedure’s specified range. CTWD is measured from the contact tip to the workpiece. |
| Travel speed | About 8–16 in/min (200–400 mm/min) can be a starting range for some short-circuit applications; joint design and position change the suitable speed. | Moving too quickly can leave a narrow bead with inadequate fusion. Moving too slowly can create an oversized bead, excessive heat input, or burn-through on thin material. | Maintain a consistent pace and confirm the bead wets into both sides of the joint without excessive buildup. |
| Torch angle and direction | For many flat-position applications, use a slight push angle of about 5–15° from perpendicular. | A steep angle can disturb shielding and alter penetration and bead shape. Poor aim can cause incomplete fusion at one side of the joint. | Point the wire at the joint and keep the angle and stickout consistent. Follow the welding procedure for position and joint type. |
| Surface cleanliness | Remove oil, paint, moisture, and heavy rust from the weld area and nearby surfaces. | Contaminants can cause porosity, inclusions, and inconsistent arc behavior even when machine settings are suitable. | Clean the joint and check that the wire and gas delivery are uncontaminated before welding. |
| How to use these values | These are illustrative starting ranges for short-circuit MIG welding, not universal settings. Actual settings depend on material thickness, joint design, wire type and diameter, welding position, equipment, and the applicable welding procedure. Make test welds and inspect them before production work. |