Navigation

The C.L. Smith Blog

What Are the Top Automated Visual Inspection Systems?

Manufacturers increasingly rely on Automated Visual Inspection Systems to protect product quality at high production speeds. These systems use cameras, controlled lighting, sensors, and software to identify defects that human inspectors may overlook. A tiny scratch, uneven seal, missing component, or incorrect label can affect customer trust and production costs.

However, choosing the top system is not simply a matter of selecting the fastest camera. Reliable performance depends on resolution, inspection speed, lighting stability, software flexibility, integration options, and maintenance support. A system that performs well on metal parts may struggle with reflective packaging or transparent materials. Real factory conditions matter.

This guide examines leading inspection technologies through practical and technical criteria. It considers detection accuracy, false rejection rates, setup time, data traceability, and ease of operator training. It also considers how systems perform beside conveyors, robotic cells, and changing product lines. Small details matter.

Professional evaluations should include controlled trials with real samples, including acceptable products and known defects. Vendor demonstrations can look impressive, yet production floors are rarely perfect. Dust, vibration, glare, and inconsistent positioning may reduce accuracy. These limits deserve attention.

There is no universal winner. The strongest choice depends on product geometry, defect type, throughput, budget, and quality requirements. Some conclusions may change after testing. That is normal. By comparing system capabilities honestly, manufacturers can choose technology that supports dependable inspection rather than promising unrealistic perfection.

What Are the Top Automated Visual Inspection Systems?

Definition and Purpose of Automated Visual Inspection Systems

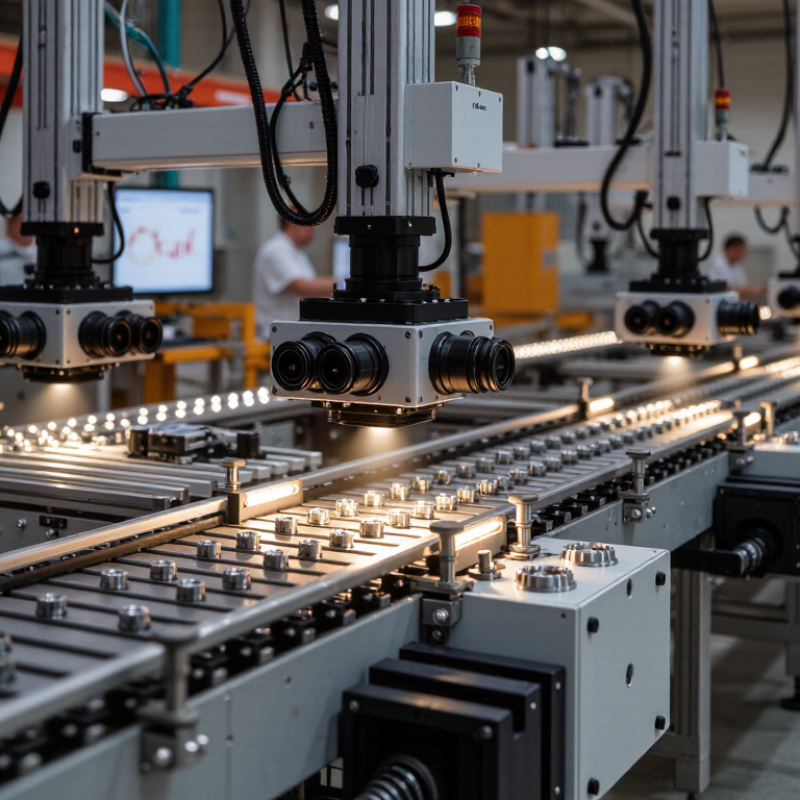
Automated visual inspection systems use cameras, lighting, software, and sensors to examine products without constant manual checking. Their purpose is practical: detect defects, verify assembly, and separate nonconforming items before shipment. A camera may identify a missing screw, uneven seal, surface scratch, or incorrect label on a moving conveyor.

The system compares each image with trained rules or reference patterns. More advanced systems use machine learning to recognize variation. This matters because factories rarely produce perfectly identical surfaces. Deloitte’s 2024 Global Smart Manufacturing Survey reported that 92% of manufacturers viewed smart manufacturing as a major competitiveness driver within three years. Automated inspection supports that goal by creating repeatable quality evidence. The International Federation of Robotics reported 541,302 industrial robots were installed globally in 2023, showing how quickly automated production environments are expanding. Yet inspection should not be treated as magic. Poor lighting, dust, vibration, and limited training images can produce false rejects or missed defects. No model is perfect.

Tips: Define the defect clearly before selecting equipment. Test samples under real production speed and lighting. Measure both false positives and missed defects. Keep human review for unusual cases, especially during early deployment. A clean demonstration can mislead. Operators should also record inspection results, maintenance changes, and recurring failure patterns. This evidence improves calibration and supports more reliable decisions over time.

Core Technologies Used in Automated Visual Inspection

What Are the Top Automated Visual Inspection Systems?

Core Technologies Used in Automated Visual Inspection

Automated visual inspection systems combine cameras, lighting, software, and production data. At the center, industrial cameras capture images at carefully controlled speeds. High-resolution sensors reveal dents, cracks, missing parts, and uneven edges. Lens selection matters too. A wide lens may distort measurements near the frame. Controlled lighting makes surface differences easier to detect. Ring lights expose scratches, while backlighting highlights gaps and incorrect outlines. Not always.

Image-processing software then converts each image into measurable information. It can compare shapes, inspect colors, and locate defects against defined limits. Machine-learning models can recognize complex patterns that rule-based inspection may miss. However, these models need representative images from real production conditions. A model trained only on clean samples may perform poorly when dust, glare, or material changes appear. That weakness requires regular testing and human review. For dimensional inspection, three-dimensional cameras can measure height, depth, and surface profile. This is useful for molded parts and assembled components.

Edge computing allows decisions to happen near the inspection station. It reduces delays and supports fast reject signals. Encoders and triggers help match each image with the correct product. Calibration records improve measurement reliability over time.

In production trials, even a small lighting shift can create false failures. I have seen stable hardware produce inconsistent results after a fixture moved slightly. That experience makes verification essential. Operators should review uncertain images, adjust thresholds carefully, and document every change.

Small defects can matter.

Main Types of Automated Visual Inspection Systems

What Are the Top Automated Visual Inspection Systems?

Main Types of Automated Visual Inspection Systems

Rule-based 2D vision systems inspect printed text, labels, surface marks, and missing components. A camera captures each item under controlled lighting. Software compares pixels, edges, colors, or shapes against preset limits. These systems work well when products remain consistent. They can struggle with glare, dust, or slight position changes.

3D inspection systems measure height, depth, and volume. They help detect uneven seals, bent parts, incomplete fills, and incorrect assembly. Structured light and laser scanning are common methods. A useful example is checking whether a cap sits two millimeters too high. Small calibration errors can still create false alarms.

AI-based vision systems learn from approved and defective samples. They can recognize complex patterns that fixed rules often miss. Deep learning is useful for scratches, stains, irregular textures, and variable assemblies. Multispectral systems add another layer by examining wavelengths beyond visible light. This can reveal moisture, coating differences, or hidden contamination. However, training data must be balanced and carefully labeled. Poor examples produce unreliable decisions. Human review remains valuable for unusual defects, especially during early deployment. Lighting should also be checked daily, not only during installation. In practice, the best system depends on product speed, defect size, surface texture, and acceptable error rates.᠎

How to Evaluate System Accuracy, Speed, and Integration

What Are the Top Automated Visual Inspection Systems?

Accuracy should be measured on real production samples, not polished demonstrations. Record false accepts, false rejects, repeatability, and performance across lighting changes. A system detecting 99% of defects may still waste time if it rejects many good parts. Use a balanced test set, including minor scratches, missing components, and normal variation. NIST measurement guidance supports separating repeatability from reproducibility during validation. That distinction is often overlooked.

Speed must match the entire line. Measure inspection time, image-transfer latency, decision time, and reject-actuator response. Do not trust camera frame rates alone. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. Inspection systems must therefore exchange data reliably with increasingly automated equipment. A fast camera is useless when downstream handling creates bottlenecks.

Integration deserves equal weight. Check communication protocols, traceability, recipe changes, cybersecurity controls, and operator training. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders viewed smart manufacturing as important for competitiveness. Yet integration projects can still fail through poor data ownership. Test the system during shift changes, product variation, and network interruptions. I would also review six months of defect data before approval. Short trials can hide maintenance costs and unstable model behavior. Perfect accuracy claims need skepticism.

Top Applications Across Manufacturing Industries

Automated visual inspection systems are changing how manufacturers detect defects, measure parts, and protect production quality. In automotive plants, cameras inspect welds, paint coverage, fasteners, and surface scratches. They can check thousands of components during one shift. Small defects matter. A missed crack may cause rework, delays, or field failures.

Electronics manufacturers use high-resolution imaging to examine circuit boards, solder joints, connectors, and component placement. In metalworking, inspection systems measure edges, holes, dimensions, and surface texture without stopping the line. Food and beverage producers apply them to packaging seals, labels, fill levels, and foreign-object detection. Pharmaceutical facilities use controlled imaging to verify printed information, container integrity, and tablet appearance. These applications require stable lighting and carefully validated inspection rules.

Packaging lines also benefit from real-time inspection. Systems can identify missing caps, damaged cartons, crooked labels, and weak seals before products leave the facility. Experience shows that automation works best when engineers combine image data with process knowledge. A camera alone is not a quality strategy. Poor lighting can create false rejects, while changing materials may confuse a trained model. Human review remains useful for unusual defects and system checks. Results should be recorded, tested, and regularly challenged. That part is often neglected. A practical installation needs clear defect definitions, maintenance routines, and operators who understand when to trust the system and when to investigate further.

What Are the Top Automated Visual Inspection Systems? - Top Applications Across Manufacturing Industries

Inspection System Core Technology Top Applications Common Defects Detected Best-Fit Industries Typical Deployment Key Strength Main Consideration
2D Machine Vision Inspection Area-scan or line-scan cameras with controlled lighting and image-processing software Surface inspection, presence and absence checks, label verification, print inspection, assembly confirmation Scratches, stains, missing parts, incorrect labels, poor print quality, color variation Automotive, electronics, packaging, food and beverage, consumer goods Inline conveyor inspection or robot-mounted inspection cell Fast, non-contact inspection for visible features Performance depends strongly on lighting, contrast, and camera positioning
3D Vision Inspection Structured light, laser triangulation, stereo vision, or time-of-flight depth sensing Dimensional verification, surface-profile measurement, bin picking, weld-bead inspection, connector and component positioning Warping, dents, incorrect height, gaps, misalignment, incomplete welds, dimensional deviations Automotive, aerospace, metal fabrication, electronics, logistics equipment Inline gauging, robotic cells, and automated material handling Measures shape and geometry that 2D cameras cannot reliably assess Reflective, transparent, or highly dark surfaces can require specialized lighting and calibration
Optical Character and Code Inspection OCR, OCV, barcode reading, and two-dimensional code verification Traceability, date-code verification, serial-number reading, packaging and regulatory information checks Unreadable characters, wrong product codes, missing codes, poor contrast, duplicated or mismatched identifiers Pharmaceuticals, medical devices, food and beverage, automotive, electronics High-speed packaging lines and final-product verification stations Supports product genealogy, recall management, and compliance controls Text quality, glare, curved surfaces, and variable print contrast affect reading reliability
Automated Optical Inspection for PCBs High-resolution 2D imaging, angled cameras, and optional 3D solder-paste measurement Bare-board inspection, component placement verification, solder-joint inspection, and assembly quality control Missing or skewed components, solder bridges, insufficient solder, lifted leads, polarity errors, and tombstoning Electronics, telecommunications, industrial controls, automotive electronics, medical electronics After solder paste printing, after placement, or after reflow Detects a broad range of assembly defects without physical contact Highly reflective solder and densely populated boards require careful optics and programming
X-Ray Inspection X-ray transmission imaging, including two-dimensional and computed tomography techniques Hidden-joint inspection, electronic assemblies, castings, batteries, packaged products, and internal structural verification Voids, cracks, porosity, broken wires, hidden solder defects, inclusions, and internal misalignment Electronics, automotive, aerospace, batteries, medical devices, metal casting Offline laboratory inspection or controlled inline production cells Examines internal features without opening or destroying the product Requires radiation shielding, safety controls, and higher capital investment
Thermal Imaging Inspection Infrared cameras and temperature-pattern analysis Electrical testing, battery inspection, heating-process monitoring, seal verification, and preventive maintenance Overheating, poor electrical connections, blocked flow, uneven heating, delamination, and abnormal thermal profiles Electrical equipment, batteries, plastics, food processing, automotive, building products Inline process monitoring or scheduled maintenance inspection Reveals heat-related conditions that may not be visible to standard cameras Emissivity, reflections, ambient temperature, and operating conditions influence measurements
Hyperspectral and Multispectral Inspection Imaging across multiple visible, near-infrared, or short-wave infrared wavelengths Material identification, contamination detection, moisture assessment, coating verification, and food-quality sorting Foreign material, moisture variation, chemical contamination, mixed materials, and coating inconsistency Food processing, pharmaceuticals, recycling, agriculture, chemicals, plastics Continuous web, conveyor, and sorting-line inspection Detects material differences that may look identical in ordinary color images Higher system complexity and data-processing requirements than conventional machine vision
AI-Based Visual Inspection Deep-learning classification, object detection, segmentation, and anomaly detection Variable surface defects, cosmetic inspection, complex assembly verification, and classification of acceptable and unacceptable products Irregular scratches, cosmetic blemishes, incomplete assemblies, unusual shapes, and difficult-to-program variations Automotive, consumer goods, electronics, packaging, pharmaceuticals, general manufacturing Inline inspection, robot cells, and quality stations with image data collection Handles complex visual patterns and can improve with representative training data Requires carefully labeled images, controlled validation, and monitoring for changes in production conditions
Selection principle: The most suitable automated visual inspection system depends on the defect type, required inspection speed, product geometry, material properties, acceptable false-reject rate, and whether the defect is visible on the surface or hidden inside the product.
Back to top