| Product Definition | Clearly specified laser film type, substrate, surface treatment, and end-use application | Technical data sheet showing whether the product is PET-based, PVC-based, PP-based, transfer film, decorative film, holographic film, or laser-marking film | “Laser film” describes several different product categories. A precise specification prevents buyers from comparing non-equivalent materials. |
| Substrate Thickness | Common PET range: approximately 12–250 μm | Thickness tolerance, measurement method, sampling plan, and independent test results | Thickness affects stiffness, dimensional stability, coating performance, converting behavior, and total material cost. |
| Thickness Tolerance | Defined tolerance stated on the product specification; tighter tolerances should be supported by process-control records | Coating-line control chart, incoming-material records, and at least three batch inspection reports | Uncontrolled thickness variation can cause wrinkles, uneven optical effects, inconsistent lamination, and waste during high-speed processing. |
| Film Width and Roll Format | Width, core size, outer diameter, winding direction, and roll length matched to the buyer’s equipment | Available width matrix, roll drawing, packaging specification, and photographs of finished rolls | Correct roll geometry reduces slitting losses, machine downtime, and compatibility problems at the converting site. |
| Optical Haze and Clarity | Target values defined according to the application; transparent decorative and overlay films normally require controlled haze and clarity | Haze and luminous-transmittance results measured according to ASTM D1003 or an equivalent recognized method | Optical uniformity directly influences visual quality, holographic brightness, readability, and defect visibility. |
| Gloss and Surface Appearance | Gloss level and visual appearance approved against a retained master sample | Gloss measurement data, defect classification standard, inspection lighting conditions, and approved limit samples | A written appearance standard is more reliable than subjective descriptions such as “high gloss” or “premium finish.” |
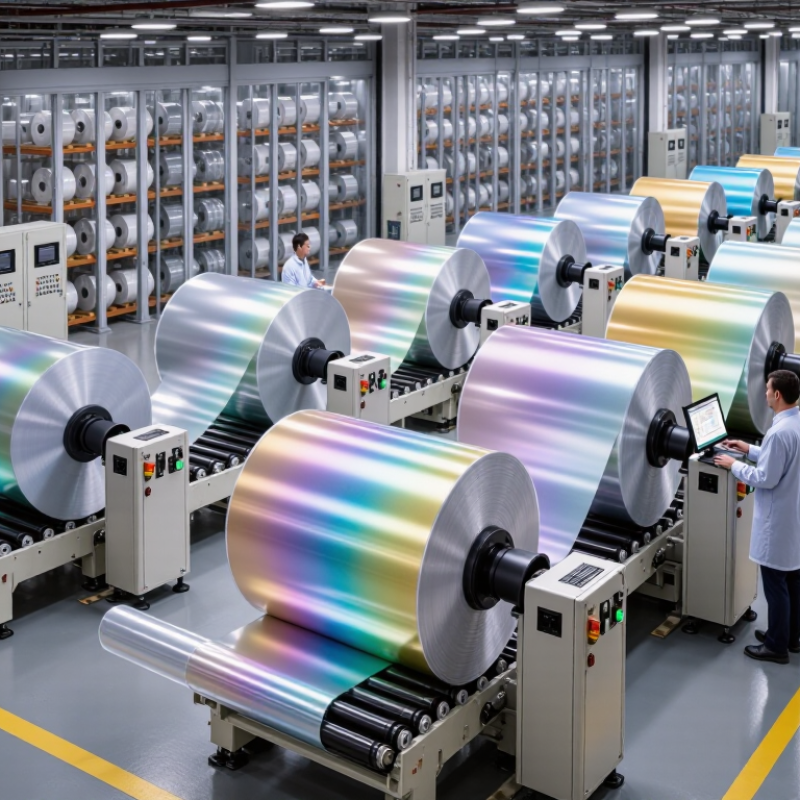
| Laser or Holographic Effect Uniformity | Consistent pattern registration, brightness, color shift, and defect rate across the usable roll length | Full-width sample, roll-start/roll-middle/roll-end inspection photos, pattern-registration records, and defect map | Uniformity across the entire roll is essential for packaging, security graphics, labels, and decorative applications. |
| Coating and Adhesion | Coating must remain attached during cutting, laminating, printing, bending, and intended environmental exposure | Cross-hatch adhesion results, tape test records, lamination trials, and technical information for the adhesive system | Poor adhesion can lead to delamination, ink failure, surface peeling, and costly customer claims. |
| Mechanical Performance | Strength, elongation, tear resistance, and dimensional stability matched to the converting process | Data generated under ASTM D882, ISO 527, or an equivalent standard, including machine and transverse directions | Mechanical data helps determine whether the film can tolerate printing, die-cutting, slitting, thermoforming, or lamination. |
| Dimensional Stability | Defined shrinkage or expansion limits after heat exposure and processing | Test temperature, dwell time, direction-specific results, and test method; for PET products, request data relevant to the intended process temperature | Dimensional change can cause registration errors, edge curl, wrinkles, and misalignment in multilayer products. |
| Printing Compatibility | Compatibility confirmed for the buyer’s printing method, such as gravure, flexographic, screen, offset, digital, or UV printing | Ink-adhesion test, surface-energy information where relevant, curing conditions, and printed trial samples | A film that performs well in one printing system may fail in another because of surface treatment and ink chemistry differences. |
| Surface Treatment | Corona, primer, hard coat, anti-static, release, or other treatment clearly identified and controlled | Surface-treatment specification, dyne-level records where applicable, treatment aging data, and storage recommendations | Surface treatment can change over time and directly affects printing, bonding, coating, and handling performance. |
| Environmental Resistance | Resistance requirements defined for humidity, heat, light, chemicals, and outdoor exposure according to the final application | Accelerated-aging reports, chemical-resistance tests, temperature range, and test duration; request ISO 4892-3 data when UV exposure is relevant | Laboratory data helps distinguish an indoor decorative product from a film suitable for demanding outdoor or long-life applications. |
| Color and Batch Consistency | Color, brightness, and optical effect controlled against an approved reference sample | Color-control records, ΔE limits where applicable, retained samples, and comparison data from multiple production batches | Stable batch performance is critical for repeat orders, coordinated packaging, and multi-site production. |
| Quality-Control System | Documented incoming, in-process, and final inspection | Inspection plan, calibration certificates, nonconformance procedure, corrective-action reports, and sample COAs | A certificate alone does not prove consistent quality. Buyers should verify how measurements are performed and how failures are handled. |
| Management Certification | ISO 9001 certification with valid scope and issuing-body verification | Current certificate, scope covering film manufacturing, certificate number, validity dates, and verification link or issuing-body record | Certification is useful evidence of a management system, but it should not replace product testing and factory qualification. |
| Regulatory Documentation | Applicable REACH and RoHS declarations supported by material records | Current declarations, restricted-substance test reports, safety data where applicable, and statements for inks, coatings, adhesives, and substrates | Regulatory compliance may involve every layer of a laminated structure, not only the base film. |
| Food-Contact Suitability | Only claim food-contact suitability when the complete structure and intended use are covered by applicable regulations | Migration testing, formulation declaration, intended-use limits, and documentation for all inks, coatings, adhesives, and substrates | A general “non-toxic” statement is not equivalent to food-contact compliance. |
| Sampling and Pilot Trial | Free or low-cost representative sample with defined sample identity | Sample lot number, production date, technical data sheet, trial guidance, and retained reference sample | Samples should be traceable to production material so that trial results can be connected to future bulk orders. |
| Minimum Order Quantity | MOQ agreed by film type, width, thickness, color, pattern, coating, and customized packaging | Formal quotation showing standard MOQ, custom MOQ, slitting charges, setup fees, and sample-order terms | MOQ can change substantially when a buyer requests a new pattern, coating, color, or special roll format. |
| Lead Time and Capacity | Lead time stated separately for standard stock, customized production, sampling, and repeat orders | Production schedule, monthly capacity statement, material-reservation policy, and recent on-time-delivery records | Capacity claims should be connected to actual line availability and the specific film construction being purchased. |
| Packaging and Export Protection | Moisture-resistant, impact-resistant, clearly labeled roll packaging suitable for international transport | Packaging specification, pallet dimensions, gross weight, loading photos, and instructions for storage and acclimatization | Improper packaging can cause telescoping, edge damage, moisture exposure, and surface contamination during transit. |
| Traceability | Each roll linked to a production lot and inspection record | Roll label format, lot-number rules, production records, COA template, and complaint-traceability procedure | Traceability enables targeted containment and root-cause analysis instead of rejecting an entire shipment. |
| Pre-Shipment Inspection | Inspection completed before dispatch against an agreed purchase specification | Pre-shipment inspection report, roll count, dimensions, appearance results, photos, and approved sampling level | Pre-shipment verification reduces the risk of receiving incorrect widths, mixed lots, damaged rolls, or nonconforming optical effects. |
| Commercial Transparency | Quotation clearly separates material price, tooling or pattern fees, slitting, packaging, testing, freight, and payment terms | Itemized quotation, Incoterms, payment schedule, validity period, warranty terms, and change-control procedure | Transparent pricing makes competing supplier offers easier to compare and reduces unexpected landed costs. |
| Recommended Qualification Decision | Approve only after document review, production sample trial, and agreed acceptance criteria | Completed supplier questionnaire, verified certificates, passed pilot trial, signed specification, and approved golden sample | The strongest supplier is not necessarily the lowest-priced option; it is the one that can repeatedly meet the buyer’s documented requirements. |